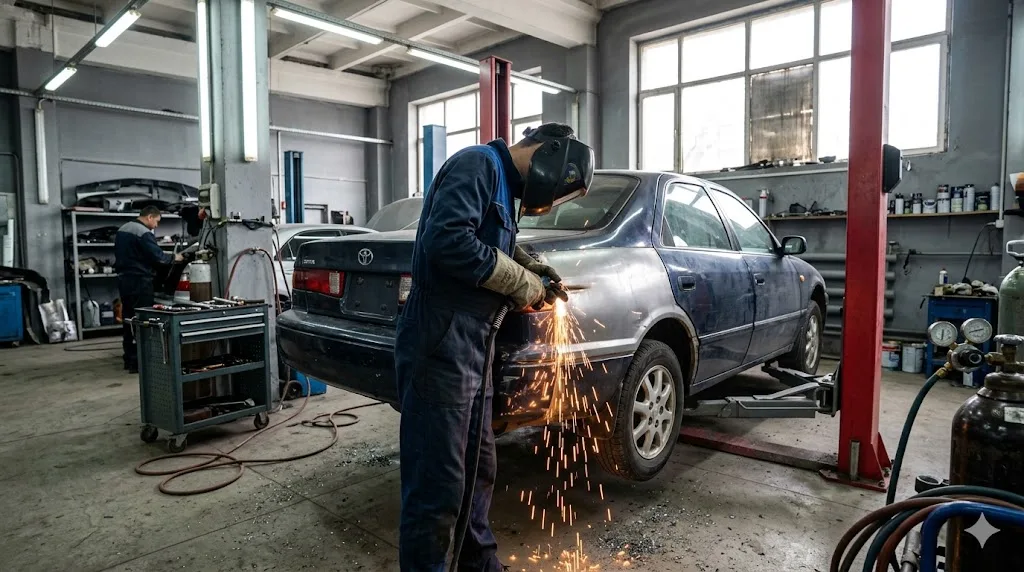
Vehicle welding in Almaty
from 3 000 KZT* per metre of joint
Rotted sill or burnt-out muffler? We weld without burning through thin metal: the arch — in 1–2 hours, the muffler without removal — in 20–40 minutes.
 Thresholds and arches
without burn-through or warping Welder visit
in 2 hours 3-year warranty
 Muffler without removal
in 20–40 minutes
Vehicle welding in Almaty
from 3 000 KZT* per metre of joint
Rotted sill or burnt-out muffler? We weld without burning through thin metal: the arch — in 1–2 hours, the muffler without removal — in 20–40 minutes.
Thresholds and arches
without burn-through or warping
Welder visit
in 2 hours
3-year warranty
Muffler without removal
in 20–40 minutes
Vehicle welding in Almaty
from 3 000 KZT* per metre of joint
Rotted sill or burnt-out muffler? We weld without burning through thin metal: the arch — in 1–2 hours, the muffler without removal — in 20–40 minutes.
Thresholds and arches
without burn-through or warping
Welder visit
in 2 hours
3-year warranty
Muffler without removal
in 20–40 minutes
Types of welding
work we do
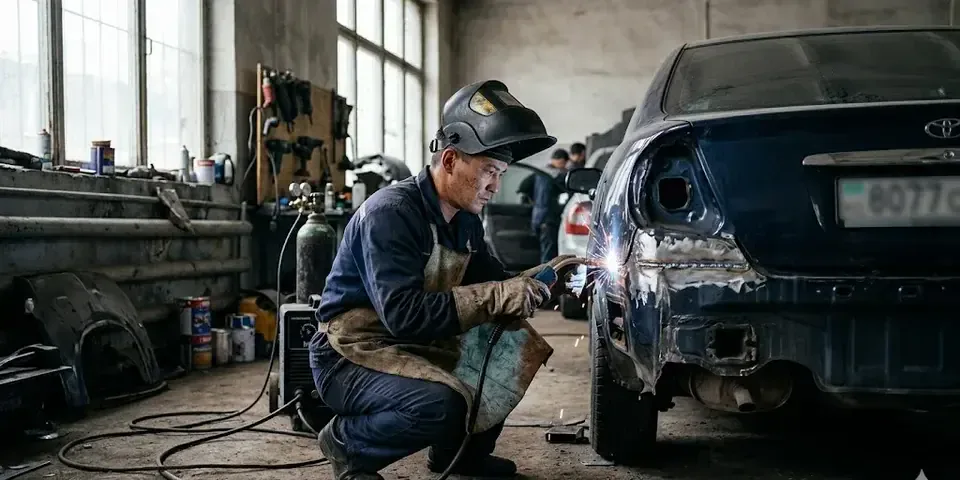
Car body repair
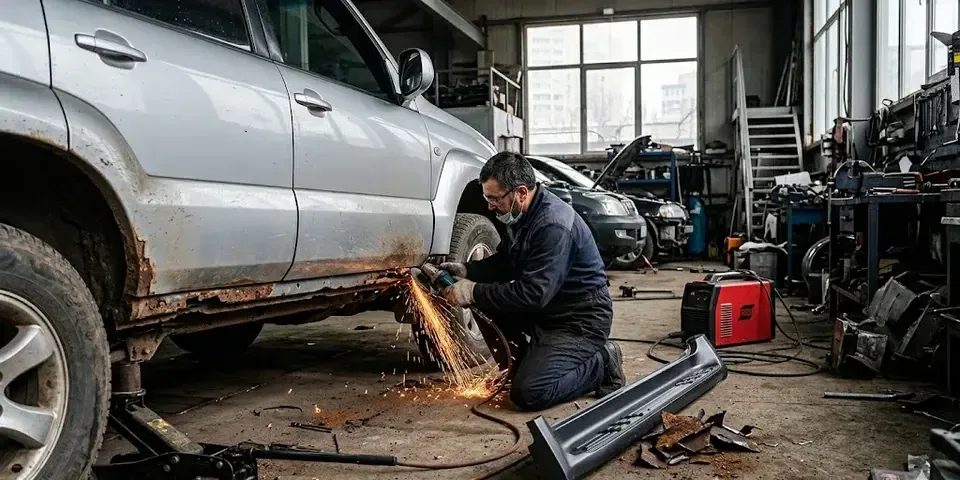
Replacing car sills
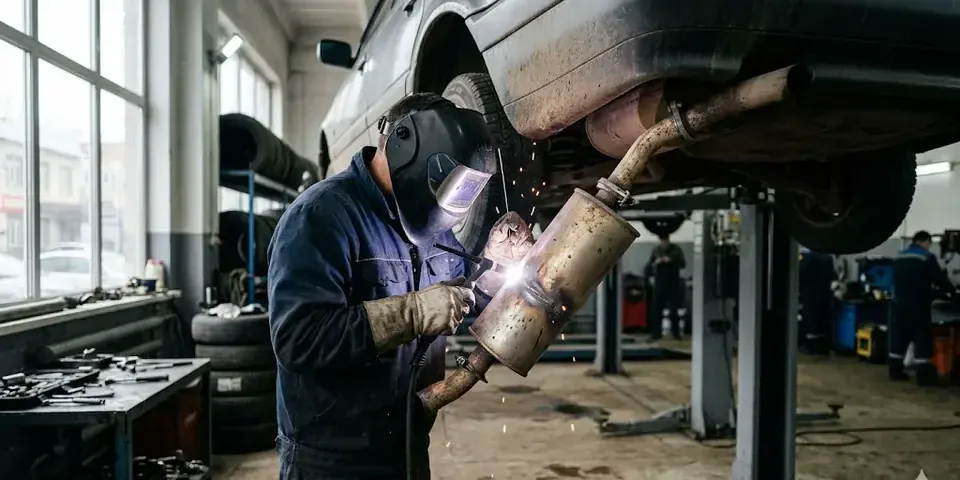
Muffler welding
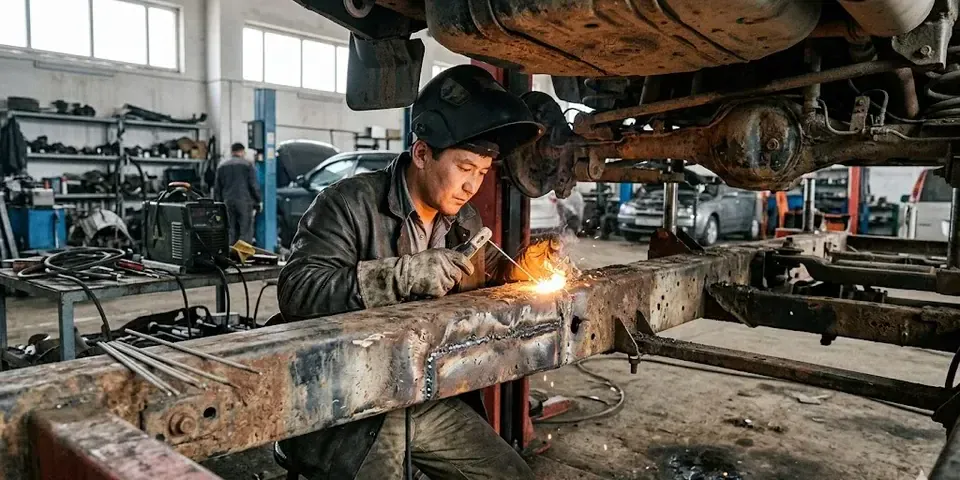
SUV frame repair
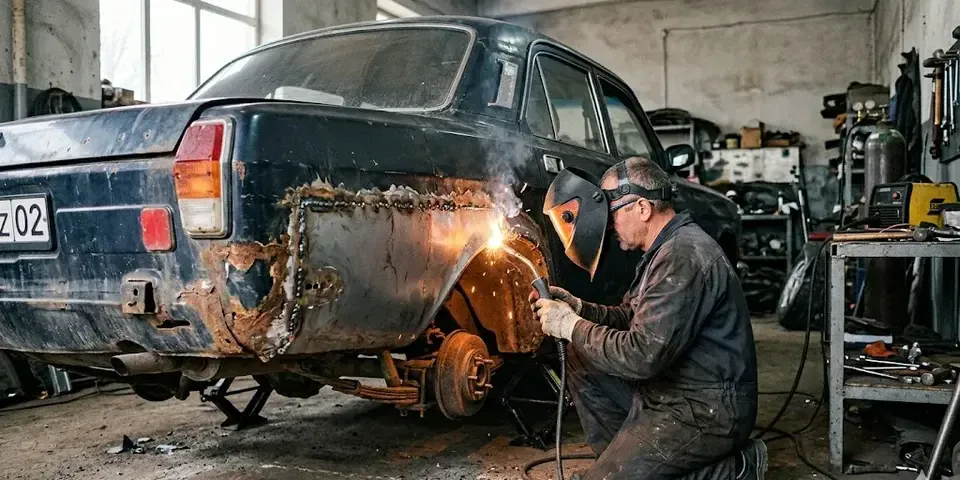
Restoration of wheel arches
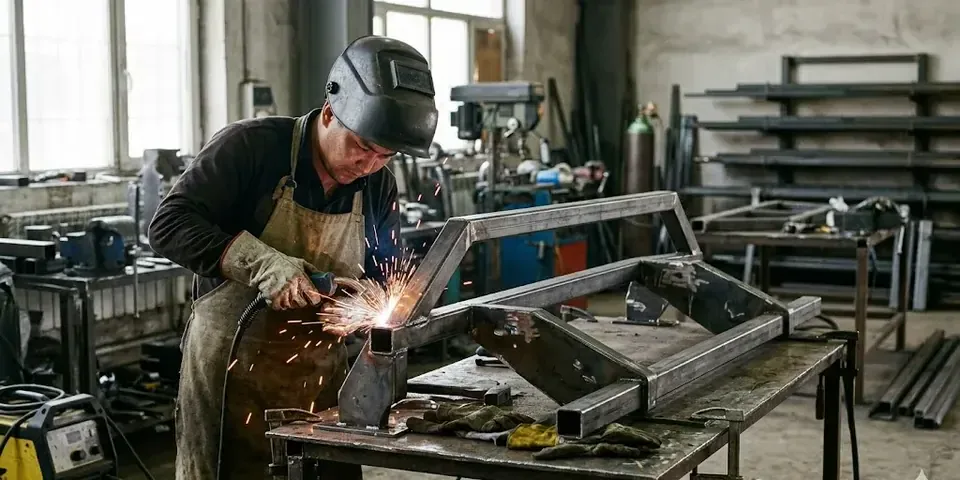
Making a bull bar
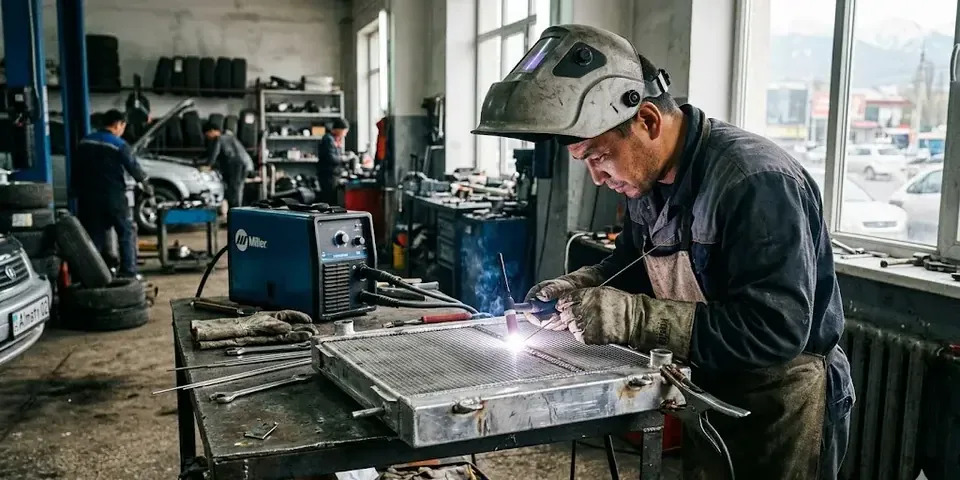
Welding of aluminium parts
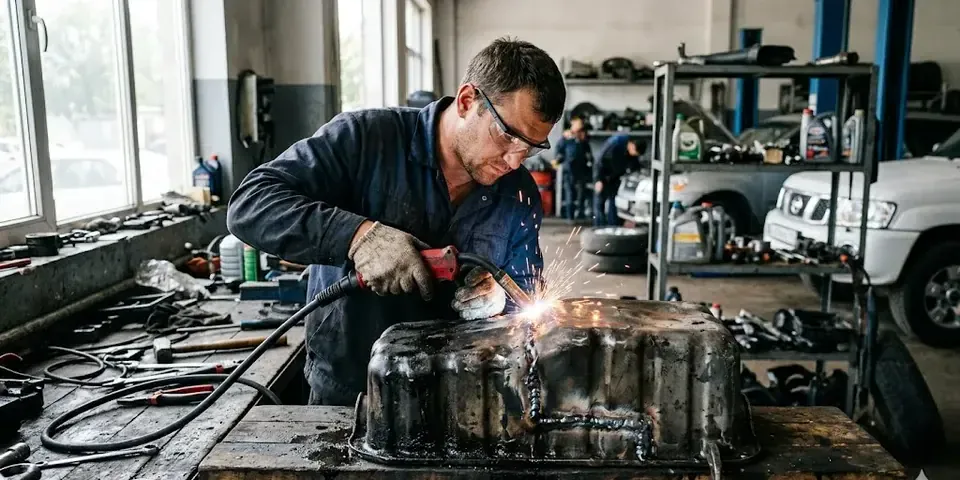
Engine sump repair
Types of welding
work we do
Car body repair
Replacing car sills
Muffler welding
SUV frame repair
Engine sump repair
Making a bull bar
Welding of aluminium parts
Restoration of wheel arches
We will call you back within 3 minutes
Types of welding
work we do
Car body repair
Replacing car sills
Muffler welding
Engine sump repair
Restoration of wheel arches
Making a bull bar
Welding of aluminium parts
SUV frame repair
We will call you back within 3 minutes
Cost of CAR WELDING
IN ALMATY
| SERVICE | COST | TIME |
|---|---|---|
| Welder call-out in Almaty | from 3 000 ₸ | from 1 hour |
| Minimum order (crack welding, tacking) | from 3 000 ₸ | from 20 min |
| Crack welding (per 1 meter of seam) | from 3 000 ₸ | from 30 min |
| Wheel arch (per element) | from 5 000 ₸ | from 1 hour |
| Muffler, burn-through up to 5 cm (argon) | from 5 000 ₸ | from 20 min |
| Welding a patch into the bottom (per patch) | from 5 000 ₸ | from 1 hour |
| Threshold, one side (per element) | from 7 000 ₸ | from 1 hour |
| Welding a tow hitch to the frame | from 7 000 ₸ | from 2 hours |
| Frame crack up to 10 cm (electrode) | from 8 000 ₸ | from 2 hours |
| Stringer, one side | from 10 000 ₸ | from 3 hours |
| Urgent repair with on-site visit (per 2–3 hours) | +30% to the price | from 1 hour |
Преимущества СВАРОЧНЫХ РАБОТ ОТ Profi‑Dom
Thresholds without burn-through 0,8 mm
We weld with a semi-automatic machine at 40–60 A using short tacks — thin metal doesn't burn through or warp
Bodyworker with 10+ years of experience
Welding in patches, side members and frames after an accident: we check the geometry against control points
Semi-automatic, argon and MMA
Argon TIG — for aluminum and stainless steel, MIG — for car body, electrode 3 mm — for frames 3–5 mm

Welder visit in 2 hours
We weld the muffler and exhaust on site in 20–40 minutes, sills and arches — in the workshop with a straightening bench
Official 3 year warranty
Warranty on seam tightness and integrity: if it leaks or cracks — we re-weld for free
Transparent price in KZT
Arch from 5 000 ₸, threshold from 7 000 ₸ — we quote the price from a photo, payment after acceptance of the work
Преимущества СВАРОЧНЫХ РАБОТ ОТ Profi‑Dom
We weld with a semi-automatic machine at 40–60 A using short tacks — thin metal doesn't burn through or warp
Thresholds without burn-through 0,8 mm
Welding in patches, side members and frames after an accident: we check the geometry against control points
Bodyworker with 10+ years of experience
Argon TIG — for aluminum and stainless steel, MIG — for car body, electrode 3 mm — for frames 3–5 mm
Semi-automatic, argon and MMA
We weld the muffler and exhaust on site in 20–40 minutes, sills and arches — in the workshop with a straightening bench
Welder visit in 2 hours
Warranty on seam tightness and integrity: if it leaks or cracks — we re-weld for free
Official 3 year warranty
Arch from 5 000 ₸, threshold from 7 000 ₸ — we quote the price from a photo, payment after acceptance of the work
Transparent price in KZT
We will call you back within 3 minutes
Преимущества СВАРОЧНЫХ РАБОТ ОТ Profi‑Dom
We weld with a semi-automatic machine at 40–60 A using short tacks — thin metal doesn't burn through or warp
Thresholds without burn-through 0,8 mm
Welding in patches, side members and frames after an accident: we check the geometry against control points
Bodyworker with 10+ years of experience
Argon TIG — for aluminum and stainless steel, MIG — for car body, electrode 3 mm — for frames 3–5 mm
Semi-automatic, argon and MMA
We weld the muffler and exhaust on site in 20–40 minutes, sills and arches — in the workshop with a straightening bench
Welder visit in 2 hours
Warranty on seam tightness and integrity: if it leaks or cracks — we re-weld for free
Official 3 year warranty
Arch from 5 000 ₸, threshold from 7 000 ₸ — we quote the price from a photo, payment after acceptance of the work
Transparent price in KZT
We will call you back within 3 minutes
HOW WE WORK
- 01.Discussion and estimate
You send a photo of the damage via WhatsApp — within 5–10 minutes we'll tell you the welding method and price.
- 02.Workshop or on-site visit
We weld the muffler on site, sills and arches — in the workshop; the welder arrives within 2 hours.
- 03.Defect inspection
We inspect the part on a lift, cut out rust down to sound metal, drill out cracks.
- 04.Price coordination
We fix the price before work begins — after inspection, the price does not change.
- 05.Metal preparation
We clean the area to a shine and fit a patch from steel of the same thickness 0,8–1,5 mm.
- 06.Welding
We weld the body with a semi-automatic at 40–60 A, aluminum and stainless steel with TIG argon, and the frame with an electrode.
- 07.Anti-corrosion protection
We treat the seam with primer and mastic — without this, rust will appear in 2–3 months.
- 08.Acceptance and payment
We show the seam, you check the work and pay upon completion: cash, transfer or Kaspi.
Find out the cost of welding your car in 1 minutes
catalogue of completed welding work
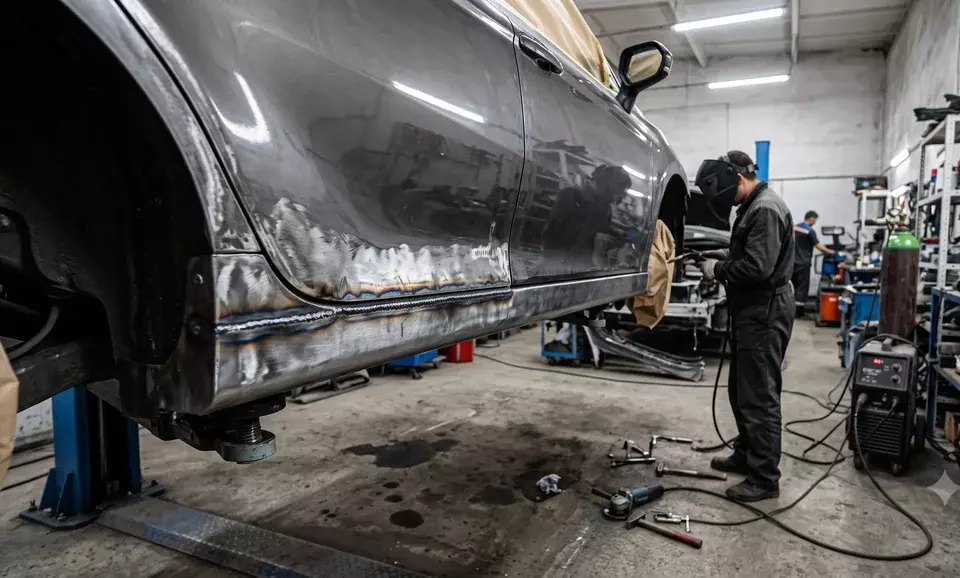 Re-welding sills on a passenger car in the Almaly district
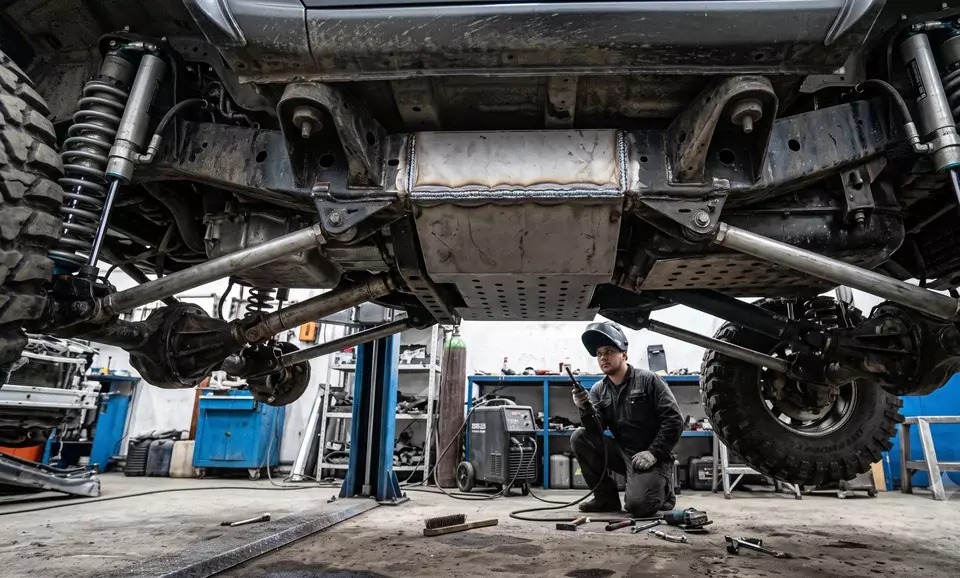 Welding of a crack on an SUV side member in Zhetysu district
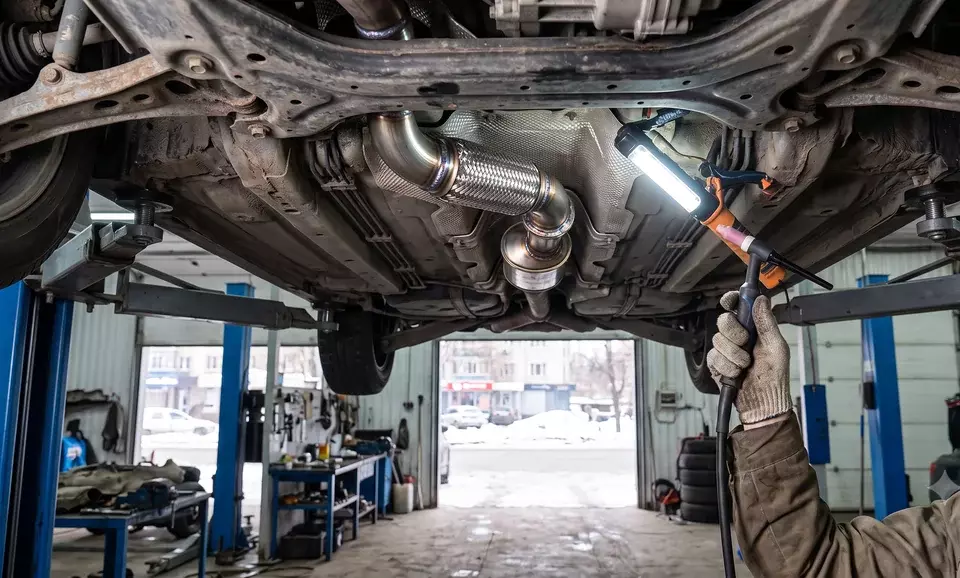 Muffler repair and flex pipe replacement in the Ainabulak microdistrict
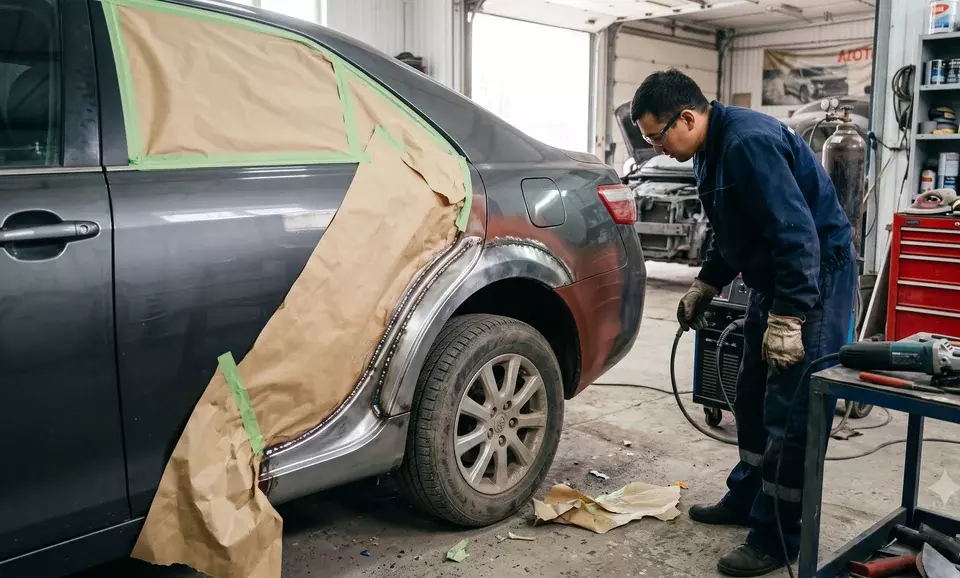 Re-welding rear wheel arches in the Medeu district

FIND OUT THE COST OF WELDING WORK FOR YOUR PROJECT
Leave a request and we will contact you within 3 minutes
Thank you! We will contact you within 3 minutes.
By clicking the button you agree to the terms of the
Or call us at
+7 (707) 068-88-68Privacy PolicyFIND OUT THE COST OF WELDING WORK FOR YOUR PROJECT
Leave a request and we will contact you within 3 minutes
Thank you! We will contact you within 3 minutes.
By clicking the button you agree to the terms of the
Or call us at
+7 (707) 068-88-68Privacy PolicyFIND OUT THE COST OF WELDING WORK FOR YOUR PROJECT
Leave a request and we will contact you within 3 minutes
Thank you! We will contact you within 3 minutes.
By clicking the button you agree to the terms of the
Or call us at
+7 (707) 068-88-68Сварка машин в Алматы от PROFI‑DOM: кузов, глушитель, рама, цены
Car welding at PROFI-DOM — body, silencer, frame and aluminium parts: MIG/MAG semi-automatic for thin body sheet, TIG argon for exhaust and aluminium. We travel around the city — from 3000 ₸, seam warranty — 3 years. Price — from 5000 ₸ per element: wheel arch, patch in the floor pan, silencer with burn-through up to 5 cm.
Published: 12 · Updated:
What and how cars are welded — MIG, TIG, spot welding
The choice of welding method directly depends on the metal, its thickness, and the specific part. Let's break down which method we use and when — from semi-automatic to argon.
MIG/MAG semi-automatic welder — the main method for body sheet metal
We weld body panels with a MIG/MAG semi-automatic welder using Sv-08G2S wire 0,8 mm in diameter — this gives a neat joint without burn-through on 0,8–1,2 mm sheet. This is exactly how we weld sills, arches, wings and the underbody: the “short arc” mode reduces heat input, so the metal does not warp. The filler wire is fed continuously, and the shielding gas (a CO₂ and argon mix or pure CO₂) blocks oxidation of the welded joint. For rusty sills or arches with corrosion, we first cut out the damaged section, then weld in a patch of steel of the same thickness — the semi-automatic welder produces an even bead with root penetration and no defects. Before working on thin body sheet, we always set the current and feed rate: on a 0,8 mm sill the current does not exceed 60–70 A, otherwise we burn through the part.
Argon TIG — for aluminium, stainless steel and thin parts
We TIG weld aluminum engine pans, radiators, intercoolers and stainless steel exhaust systems with argon — the joint comes out hermetic, without scale or spatter. For aluminum we use ER4043 (AlSi5) filler, for stainless steel — ER308L; we weld aluminum with alternating current (AC) at a cleaning balance of 70/30. TIG welding produces no sparks or spatter, so it is used for decorative muffler elements and thin-walled air conditioner tubes. The main difference from semi-automatic welding is that the welder guides the arc with one hand and feeds the filler with the other, which requires high qualification. Before working with aluminum, we always clean the part with a stainless steel brush and degrease with acetone — if the oxide film is missed, pores will remain in the weld joint and the connection will leak.
Spot welding (spotter) and MMA — for panel beating and frames
We use a spot welder to tack body panels during panel beating and to spot-weld factory joints on sills, and we use MMA electrode welding to weld SUV frames and subframes — for thick metal from 3 mm this is more reliable than a semi-automatic. The spot welder works with a current pulse of 5000–8000 A, welding a back-up washer or electrode to the dent — after pulling, the washer is knocked off and the mark is ground down. For frame cracks on a Toyota Land Cruiser or UAZ we use UONI-13/55 electrodes with a diameter of 3–4 mm: they give deep penetration and a ductile joint that withstands impact loads. MMA welding is not used on thin body sheet (0,8–1,5 mm) — the arc burns through the metal. When working on a frame it is important to drill the ends of the crack with a 3–5 mm drill bit to stop it from growing, otherwise the weld will crack next to it.
How to tell that welding has been done well
- Even bead: the bead width is the same along its entire length, with no ridges or dips — this indicates a stable arc travel speed.
- No porosity or craters: the surface is dense, with no pinholes or blowholes — which means the gas shielding was not disrupted and the metal was clean.
- No undercutting: the base metal is not thinned next to the welded joint — undercutting weakens the part and leads to cracking under load.
- Cleaning and anti-corrosion treatment: the weld area is brushed, scale is knocked off and an anti-corrosion compound is applied — without this, rust will set in within six months.
Body repair by welding — sills, wheel arches, longitudinal beams, underbody
Body repair is the most common reason car owners look for welding services at a service station. Let's break down how we weld sills, arches, longitudinal beams, and the underbody without burn-through or panel distortion.
Sill welding — without burning through thin metal
We weld sills with a semi-automatic welder at minimum current — using spot tacks so as not to overheat the metal or burn through it. Thin body sheet (0,6–0,8 mm) on the sills of a Kia Rio, Hyundai Accent or Lada Vesta requires tack spacing of 10–15 mm with the seam cooling between passes: we use a MIG/MAG semi-automatic welder with 0,6–0,8 mm wire and CO₂+Ar gas, and set the current to 40–60 A. Before work we always clean the area down to shiny metal — if paint or filler is left behind, the welded joint will be porous and only half as strong. If the sill is rusted right through, we cut out all the rust back to sound metal and weld in a patch of the same sheet — we do not “patch” over rot.
Welding in arches and patches in the underbody — with anti-corrosion treatment
We weld the wheel arch in 1–2 hours: cut out the rust, straighten, weld in a patch and immediately treat with anti-corrosion compound. On the arches of Toyota Camry or Mitsubishi L200, corrosion most often starts from the wheel arch liners — we have to remove the plastic, cut out the source and fit the patch to the arch radius. Straightening before work is mandatory: if the arch has been bent by an impact, we first straighten it on the frame machine, otherwise the patch will sit crooked and the door will catch. After welding the patch into the underbody, we обязательно treat the seam with mastic and primer — otherwise corrosion will start from the back side within a season.
Restoring longitudinal beams after an accident — checking for warping
We restore chassis rails after accidents using a semi-automatic welder with mandatory geometry checks — so the body does not warp. A front-end impact on a Mercedes W210 or BMW E39 often crumples the chassis rail like an accordion: we cut out the deformed section, straighten the edges and weld in a reinforced patch made of 1,2–1,5 mm steel. A semi-automatic welder with 0,8–1,0 mm wire gives full-thickness penetration without undercutting — this is critical for the structural frame. Before working on a chassis rail, we check the dimensions against the reference points — if it has warped, we straighten it on a jig first, then weld.
Is painting needed after body welding
After welding, painting is mandatory — an uncoated welded joint will begin to rust in 2–3 months, especially in Almaty with humidity fluctuations. Welding scale is an active corrosion center: if left as is, in six months a rust spot will appear under the welded joint, and in a year — a through hole. Painters prime the seam with an acid primer, then putty the transition and paint it to match the body color — the full cycle takes 1–2 days. If you do not plan to paint immediately, at least prime the welding area — this will protect it for a month or two until you get to the painter.
Muffler and exhaust repair — stainless steel, burn-through, flex pipe
Burn-through of a silencer is a problem many car owners across Almaty face. Let us explain when it is worth welding and when it is easier to buy a new component.
Can a muffler be welded without removing it
Yes, we weld a muffler without removing it — with TIG argon if the burn-through is accessible from below on a lift, and with a MIG semiautomatic if the part can be moved 5–7 cm away from the body. For stainless steel we use argon back purging on the reverse side of the seam, otherwise the welded joint darkens and loses its corrosion resistance. On the exhaust systems of a Toyota Camry 40–50 and Mitsubishi L200 access to the muffler is usually open — we weld it in 30–40 minutes without removal. If the muffler is removed, the result is better: we weld it from all sides and treat it with anti-corrosion compound, but we also work without removal if that is more convenient for the client.
What to do if the silencer has burned through — weld or replace
If the burn-through is small (up to 3–5 cm) and the surrounding metal is not rotten, we weld with TIG argon using a stainless filler. If the muffler has rusted through along a seam or its entire length, it is cheaper to buy a new one: a new muffler for Daewoo Nexia or VAZ costs -2110 — 5–8 thousand ₸, and replacement work — 3–5 thousand ₸. For foreign cars (Hyundai Accent, Kia Rio) a new muffler costs 12–18 thousand ₸ — welding burn-throughs starts from 5 thousand ₸. Clients often think a muffler 'can't be welded', but TIG argon gives a hermetic joint — this is more cost-effective than a new one at 20–30 thousand ₸ on complex models.
Repair of the flex pipe, resonator and downpipe
We repair exhaust corrugations without removing the muffler — with TIG argon and back purging so the joint is airtight and does not crack from vibration while driving. At PROFI-DOM, for corrugations we use ER308L stainless wire — it withstands heating up to 800 °C and does not crack in frost. The resonator and downpipe on Mercedes W210 and BMW E39 are often welded with a MIG semi-automatic due to the 2–3 mm metal thickness.
Stainless steel exhaust welding — key features
Stainless steel is welded with argon using TIG with a stainless wire filler and argon purging from the back side — the joint is strong and does not rust. For AISI 304 and 409 exhaust pipes, we use ER308L wire: it produces a ductile seam that withstands vibration on the Almaty — Kapshagay highway. The metal thickness on factory Hyundai and Kia mufflers is 1,2–1,5 mm, on Chinese analogues — 0,8–1 mm; they burn through even at the minimum current of 40 A. Ordinary steel wire is not suitable for stainless steel — the joint will quickly rust from condensation.
Frames, brackets, tow bars, fuel tanks — critical components
Welding load-bearing body elements and specific parts requires a special approach and the right equipment. Let us look at four difficult scenarios that bring people to us most often.
Welding cracks in an SUV frame — will it hold
We weld a crack in the frame with MMA electrode welding with mandatory edge preparation — the joint withstands the load no worse than a factory one, if the metal is not rusty. To do this, we chamfer along the crack to the full depth so that the electrode welds the root of the seam rather than lying on top as a "patch". We use UONI-13/55 electrodes with a diameter of 3 mm — they produce a ductile seam that withstands impact loads on the frame. The frame thickness on SUVs is 3–5 mm, so we weld with a 3 mm electrode on reverse polarity, current 90–120 A. Before welding, we обязательно drill the ends of the crack with a 5 mm drill — this stops its growth through the metal, otherwise in a month a new branch will appear next to the seam.
Welding a tow bar to the frame — which welding method is best
We weld the tow bar to the frame with a MIG/MAG semi-automatic welder — the joint comes out strong and elastic, withstanding a static load of up to 2 tons without risk of tearing off. A 0,8 mm wire in a CO₂ environment provides deep penetration without overheating the frame metal, which is especially important on thin-walled frames of Mitsubishi L200 and Toyota Hilux (4–5 mm). The weld length is at least 60 mm on each side of the tow bar platform, with two crosswise passes so the load is distributed evenly. If the tow bar is bolted on but one hole has torn out, we weld it up and drill a new one nearby. This costs 3–4 times less than a new tow bar, and in strength it is not inferior to the factory mounting.
Welding of aluminium parts — sump, radiator
We weld aluminum oil pans and radiators with TIG argon using ER 4043 — filler — the joint is hermetic, does not leak and withstands oil pressure up to 3–4 bar. On the engine pan of a 2JZ-GE (Toyota Mark II), the wall thickness is 1,5–2 mm, so we work with a current of 70–90 A, a 2 mm tungsten electrode and a 2,4 mm filler rod. Before welding, we must preheat the part to 150–200 °C with a gas torch — otherwise, due to the temperature difference, the seam will crack when cooling. Without preheating, even a quality joint gives 1–2 % shrinkage and tears the base metal around the weld zone. Aluminum is a capricious metal: cleaning from oil with a solvent and drying before preheating are mandatory, otherwise pores in the seam are guaranteed.
Fuel tank welding — safety and steaming
We only weld a fuel tank after mandatory steaming — we evaporate the remaining petrol with steam for 30–40 minutes to rule out a vapour explosion. Even an empty tank is dangerous: petrol vapour in a confined volume is explosive at a concentration of 1,4–7,6 % in air. Steaming is done through the filler neck — we supply steam from a steam generator, the tank heats up inside to 100 °C, and all the vapours are displaced outside. After that we measure the residual concentration with a gas analyser — only when the readings are zero do we start TIG argon welding at a minimum current of 50–60 A. We run the joint on a 0,8–1 mm thick tank with short tacks of 10–15 mm, letting the part cool between passes so as not to burn through the wall.
Car welding price — per element, call-out, emergency repair
The cost consists of the part, welding method and scope of work. Below is the price list for popular elements, visits and urgent orders.
How much does welding sills, wheel arches and a silencer cost
| Work / element | Welding method | Unit | Price from, ₸ |
|---|---|---|---|
| Sill (one side) | MIG/MAG semi-automatic welder | element | 7 000 |
| Wheel arch | MIG/MAG semi-automatic welder | element | 5 000 |
| Muffler (burn-through of up to 5 cm) | Argon TIG | element | 5 000 |
| Muffler (burn-through of more than 5 cm) | Argon TIG | element | 7 000 |
| Welding a patch into the underbody | MIG/MAG semi-automatic welder | patch | 5 000 |
| Longitudinal beam (one side) | MIG/MAG semi-automatic welder | element | 10 000 |
| Frame (crack up to 10 cm) | MMA (electrode) | weld | 8 000 |
| Tow bar (welding on) | MIG/MAG semi-automatic welder | element | 7 000 |
| Aluminium sump | Argon TIG | element | 10 000 |
| Fuel tank (steam cleaning + welding) | Argon TIG | element | 12 000 |
Price per weld and patch — alternative options
Welding a crack up to 10 cm on a bracket or exhaust pipe costs from 3000 ₸ per linear meter — this is cheaper than replacing the unit entirely. Welding a patch onto a rotten section of the underbody or wheel arch — from 5000 ₸ per piece, with cutting and on-site fitting. The difference between a seam and a patch is the amount of rust: if the metal around the crack is thin, the craftsman cuts out the section and installs a patch, otherwise the joint will separate within a month. Before welding a crack on an aluminum pan, diagnostics are needed: if the crack runs along the joint, the price will be lower than on the body of the part.
Cost of a call-out and a tow truck
Welder's visit in Almaty — from 3000 ₸ within the city. If the car is not driveable — tow truck from 5000 ₸ around the city. A visit is convenient for a muffler or exhaust pipe — the master arrives with argon and welds on site in the yard or parking lot. But for body repair of sills or wheel arches, a workshop is better: it has a frame machine to fix the geometry, sandblasting to clean rust, and anti-corrosion treatment after welding — such equipment is not available on a visit.
Urgent repairs and minimum order
Urgent repair with on-site visit — a surcharge of 30% on top of the work price, done within 2–3 hours of the call. Minimum order — from 3000 ₸, which is one weld of a crack on a muffler or tacking a bracket. An urgent order is relevant if the car is needed tomorrow morning — for example, the muffler fell off on Friday evening and there's a trip to the dacha on Saturday. The urgency surcharge is not included in the tow truck cost — if the car is not drivable, the tow truck is paid separately.
How to order welding and a call-out across Almaty
Ordering car welding in Almaty is simple: one call or message — and the specialist is already on the way. Here is how the process looks from the call to the finished part.
How we work — from the call to the finished part
By phone call or WhatsApp message, the craftsman clarifies the part, welding method and preliminary price within 5–10 minutes. If a site visit is needed, the welder arrives within 2 hours at any address, inspects the damage on site and agrees the final cost. For body parts (sills, arches, side members), welding takes from 40 minutes to 3 hours depending on the degree of corrosion. We weld a muffler or flex pipe in 20–40 minutes without removal — right on the car, after which the joint is cleaned and primed. For an exact price, a photo of the part via WhatsApp is enough — so you immediately know how much it costs and when it will be ready, without extra trips and inspections at the service center.
Call-outs by district — where we work
We travel to all districts: Bostandyk, Almaly, Auezov, Medeu, Turksib, Zhetysu, Nauryzbay, including remote microdistricts Aksai, Alatau, Shanyrak, Koktobe, Kamenskoye Plato. Travel to the suburbs up to 30 km from the city limits is also possible — we agree on the cost in advance, and within the city travel is from 3 000 ₸ with no extra charge for mileage. If you live in Guldala or Irgeli, travel time increases to 1–1,5 hours, which should be taken into account in advance.
Warranty on welding work
PROFI-DOM gives a 3-year warranty on all welding work: on mufflers and exhaust (TIG argon) — for seam tightness, on body elements (MIG semi-automatic) — for the absence of cracks, on load-bearing units (side members, frame) — provided anti-corrosion treatment after welding. If a seam leaks or a crack appears in the metal, we re-weld for free, without additional charge for the visit.
How to pay — cash, transfer, Kaspi
Payment by cash, card transfer, Kaspi QR or Kaspi transfer — whichever is convenient for you, no prepayment is required, you pay upon acceptance of the work. For legal entities and service stations, we issue a signed and stamped work completion certificate — we work with organizations by bank transfer, and for individuals a receipt or a screenshot of the transfer is enough to confirm the warranty.
Conclusion
Car welding is not a one-size-fits-all service: every part and metal requires its own approach and equipment. Here is the main thing to remember before ordering.
Key takeaways
- The choice of welding method depends on the metal and the part: MIG semiautomatic — for thin bodywork metal (sills, arches), TIG argon — for aluminium and stainless steel exhaust, MMA — for frames and subframes.
- Body repair requires protection against burn-through: the specialist makes spot tacks at minimum current and always cuts the rot back to sound metal — otherwise the seam will blister within a month.
- It is advantageous to weld a muffler with a small burn-through of up to 5 cm: TIG argon gives a hermetic seam, while a complete muffler replacement will cost 3-4 times more.
- The price of welding is made up of the part and the complexity: from 5000 ₸ for a silencer to 12 000 ₸ for a fuel tank with mandatory steaming — skimping on steaming is explosive.
- A mobile visit around Almaty is a convenient option for a muffler and exhaust, but bodywork repairs are better done in the workshop with subsequent anti-corrosion treatment: sills without anti-corrosion treatment in local salt will rot away in a single season.